© 2025 Messer Cutting Systems, Inc.
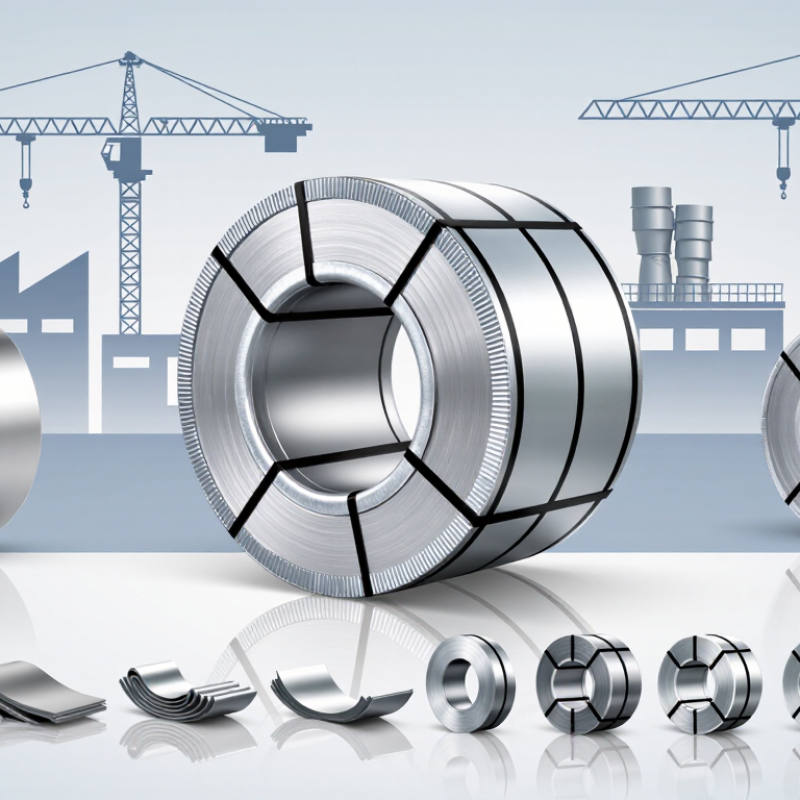
Choosing the right steel product affects construction quality, maintenance costs, and long-term reliability. Hot Dip Galvanized Steel Coil is widely selected because it combines steel strength with zinc-based corrosion protection. During production, cleaned steel passes through molten zinc, creating a bonded coating around its surface. This process protects exposed areas and helps slow rust formation in demanding environments.
In real projects, the advantages become visible over time. A galvanized coil can support roofing panels, wall systems, ventilation parts, automotive components, and fabricated structures. Its bright surface also offers a clean, consistent appearance. However, appearance alone should not guide the purchase. Experienced buyers check coating mass, steel grade, thickness tolerance, surface condition, and edge quality. Mill certificates and inspection records provide useful evidence. Traceability matters.
Small details matter.
The correct product depends on climate, forming requirements, load conditions, and expected service life. Coastal air, industrial moisture, and repeated condensation may require different protection levels. Galvanizing is durable, but it is not permanent. Cut edges, deep scratches, trapped water, and incompatible contact metals can reduce performance. Designers should provide drainage and avoid unnecessary surface damage during fabrication. Suppliers should explain applicable standards, testing methods, packaging, and storage recommendations clearly. A careful comparison may reveal that the cheapest coil is not the most economical choice. It is also fair to admit that product selection is sometimes imperfect, especially when project conditions change. A reliable decision combines technical data, practical experience, supplier credibility, and honest risk assessment.
Hot dip galvanized steel coil is carbon steel coated with a protective layer of zinc. It is produced through a continuous process. The steel strip is cleaned, heated, and passed through molten zinc, usually near 450°C. Zinc bonds with the steel surface and forms several alloy layers. A controlled cooling stage then stabilizes the coating.
This structure helps protect the steel from moisture, oxygen, and many outdoor pollutants. If the surface is scratched, zinc can provide limited sacrificial protection around the exposed area. That is one reason this coil suits roofing panels, ductwork, automotive parts, and agricultural equipment. Its smooth, bright appearance can also support later painting or forming.
A thicker zinc layer usually offers longer corrosion resistance, but it can affect welding, bending, and surface appearance. Buyers should check coating mass, steel grade, dimensional tolerance, and edge condition before ordering. In practical inspections, uneven spangle, bare spots, or oil stains may reveal processing problems. Galvanized coil is useful, but it is not a perfect answer for every environment. Constant salt spray, trapped water, or damaged cut edges still require thoughtful design and maintenance.
Why Choose Hot Dip Galvanized Steel Coil?
How Is Hot Dip Galvanized Steel Coil Manufactured?
Hot dip galvanized steel coil begins with carefully cleaned steel strip. The strip passes through alkaline cleaning, pickling, and fluxing stages. Each stage removes oil, rust, and surface scale. The line then dries the strip before entering a zinc bath near 450°C. This temperature allows molten zinc to bond with the steel surface.
Inside the bath, controlled rollers guide the moving strip. Air knives remove excess zinc and regulate coating thickness. Common coatings range from about 50 to 300 g/m², depending on the intended application. The strip then cools, levels, and receives surface treatment. Operators inspect coating weight, appearance, width, and mechanical properties.
The International Zinc Association reports that galvanizing consumes roughly 60% of global zinc demand. That figure shows its importance in corrosion protection. Meanwhile, the World Steel Association recorded about 1.89 billion tonnes of crude steel production in 2023. Even a small improvement in coating control can affect large material volumes.
The process is precise, but not flawless. A slightly dirty surface may create bare spots or uneven zinc layers. I have seen production teams adjust line speed after checking a dull patch under inspection lights. That practical judgment matters. Laboratory data helps, but real coils still require careful observation. Standards such as ASTM A653 and ISO ัน?
Key performance characteristics, typical process conditions, and quality considerations for continuously hot-dip galvanized steel coil
| Category | Dimension or Process Stage | Typical Data or Range | Why It Matters | Manufacturing and Quality Notes |
|---|---|---|---|---|
| Product Definition | Coating method | Continuous immersion of a moving steel strip in a molten zinc bath | Creates a metallurgically bonded zinc coating | The process is commonly known as continuous hot-dip galvanizing and is covered by product standards such as EN 10346 and ASTM A653/A653M. |
| Base Steel | Steel substrate | Low-carbon or HSLA steel, selected according to forming and strength requirements | Determines tensile strength, yield strength, elongation, weldability, and formability | Typical applications include construction panels, roofing, automotive parts, appliances, ducts, and general fabrication. |
| Surface Cleaning | Alkaline cleaning and rinsing | Removes oil, grease, dirt, and rolling residues | Improves wetting and helps prevent bare spots or coating defects | Cleaning effectiveness is controlled through bath concentration, temperature, contamination level, and rinse-water quality. |
| Surface Preparation | Pickling | Acid treatment removes rust and mill scale before galvanizing | Exposes a chemically active steel surface for zinc bonding | Over-pickling can roughen or excessively dissolve the substrate, so acid strength, temperature, and residence time are controlled. |
| Fluxing | Flux application and drying | Often uses a zinc-ammonium-chloride-based flux system | Reduces re-oxidation and promotes contact between clean steel and molten zinc | In continuous galvanizing lines, surface activation is commonly integrated with controlled furnace-atmosphere processing. |
| Annealing | Strip heating before the zinc bath | Temperature and soaking time depend on steel grade and required mechanical properties | Controls recrystallization, strength, ductility, and surface condition | A controlled reducing atmosphere is used to limit oxidation before the strip enters the zinc bath. |
| Zinc Bath | Molten zinc temperature | Approximately 445–465°C for a conventional zinc bath | Allows the strip to be wetted and coated while maintaining stable bath conditions | Bath chemistry and temperature influence coating appearance, adhesion, dross formation, and surface quality. |
| Zinc Coating | Coating designation | Common designations include Z100, Z180, Z275, and higher coating masses depending on the applicable standard | Higher coating mass generally provides greater zinc reserve for corrosion protection | For many standards, the designation represents the total minimum coating mass on both sides, expressed in g/m². Exact requirements depend on the standard and coating class. |
| Coating Thickness | Approximate zinc thickness | About 7 µm per side for a total coating mass of 100 g/m²; about 19 µm per side for 275 g/m² | Provides a practical way to relate coating mass to physical zinc thickness | Approximate conversion assumes a zinc density of about 7.14 g/cm³. Actual measurements vary with coating distribution and test method. |
| Coating Control | Air-knife wiping | High-pressure gas jets remove excess molten zinc and regulate coating mass | Enables more uniform coating thickness across the strip width | Air-knife pressure, nozzle-to-strip distance, strip speed, bath level, and edge effects are important process variables. |
| Surface Finish | Spangle appearance | May be minimized, regular, or visually controlled depending on product requirements | Influences appearance, painting behavior, and suitability for exposed applications | Surface appearance is affected by bath chemistry, cooling conditions, wiping practice, and post-treatment. |
| Cooling | Strip cooling after coating | Controlled gas or water-assisted cooling may be used after zinc wiping | Solidifies the zinc layer and stabilizes the final surface structure | Cooling must be controlled to avoid surface damage, uneven appearance, or distortion of the strip. |
| Post-Treatment | Passivation, oiling, or alternative surface treatment | Selected according to storage, forming, painting, and environmental requirements | Helps reduce white rust during storage and may improve subsequent processing | Post-treatment compatibility should be confirmed before painting, welding, adhesive bonding, or deep forming. |
| Corrosion Protection | Zinc barrier and sacrificial action | Zinc protects the steel by acting as a physical barrier and preferentially corroding when exposed | Provides durable protection against atmospheric corrosion | Service life depends on coating mass, environment, drainage, salt exposure, temperature, damage, and maintenance conditions. |
| Edge Protection | Cut-edge behavior | Zinc can provide limited sacrificial protection near small exposed steel areas | Helps slow corrosion around minor scratches and cut edges | For severe exposure or large damaged areas, suitable edge sealing, paint systems, or repair coatings may still be required. |
| Formability | Bending, stamping, and roll forming | Depends mainly on the selected steel grade, coating mass, surface treatment, and forming radius | Allows galvanized coil to be converted into panels, profiles, ducts, and formed components | Forming trials are recommended for demanding applications, especially with high-strength grades or tight radii. |
| Weldability | Resistance and arc welding | Generally weldable with suitable procedures, though zinc affects electrode wear, fumes, and process settings | Supports fabrication of galvanized assemblies | Ventilation, welding parameters, electrode maintenance, and applicable safety procedures are essential. |
| Inspection | Typical quality checks | Coating mass or thickness, surface appearance, dimensions, mechanical properties, adhesion, and coil condition | Confirms compliance with purchase specifications and the applicable product standard | Test methods and acceptance criteria should be agreed before production because requirements vary by standard and application. |
| Storage | Protection from wet storage stain | Store indoors in a dry, ventilated area; prevent condensation and trapped moisture | Reduces the risk of white rust and surface staining | Coils should be protected from rain, direct water contact, rapid temperature changes, and prolonged high humidity. |
| Main Advantages | Overall selection benefits | Corrosion resistance, consistent coating, recyclability, process efficiency, and broad fabrication compatibility | Offers a practical balance of durability, cost, and manufacturing performance | Selection should consider steel grade, coating designation, surface finish, dimensions, forming requirements, exposure environment, and end use. |
Reference basis: Typical values are industry ranges and examples for continuously hot-dip galvanized steel coil. Final requirements should be verified against the applicable edition of EN 10346, ASTM A653/A653M, ISO 3575, or another specified product standard.
Hot-dip galvanizing protects steel coil through a bonded zinc coating. During production, cleaned steel passes through molten zinc, creating layered protection on its surface. This bond is stronger than a simple painted film.
Zinc forms a physical barrier against moisture, oxygen, and many common contaminants. More importantly, it provides sacrificial protection. If a small scratch exposes the steel, nearby zinc corrodes first and helps shield the exposed area. That feature is valuable during cutting, transport, and installation. Small damage does not always become immediate rust.
Zinc also reacts with air and water to form a thin, stable patina. This patina slows further corrosion. The protection can remain effective for years, depending on coating thickness and exposure conditions. It is not magic. Salt spray, standing water, acidic fumes, and poor drainage can shorten service life. Cut edges and drilled holes deserve careful inspection. They are often overlooked.
In practical quality control, inspectors should check coating appearance, adhesion, thickness, and surface continuity. A reliable specification should match coating mass to the intended environment. Galvanized steel can resist abrasion during handling, but harsh contact may still damage the surface. That detail is easy to forget. Good design, proper storage, and regular inspection work together with zinc protection.
Hot dip galvanized steel coil is used where steel must face moisture, handling, and daily wear. Its zinc coating protects the underlying steel from rust. In construction, fabricators form it into roofing panels, wall cladding, door frames, gutters, and light structural sections. A cut coil can become cable trays, ventilation ducts, or warehouse shelving. The bright surface also supports clean-looking interior and exterior designs.
Agricultural buildings use galvanized coil for livestock panels, grain equipment, fencing, and water-resistant partitions. Automotive and appliance manufacturers shape it into brackets, body components, housings, and internal supports. Solar mounting structures, roadside equipment, and storage racks also depend on its practical corrosion resistance. In coastal areas, however, the coating needs careful specification. Salt exposure can shorten service life.
From workshop experience, the coating remains valuable after bending, but poor forming can damage edges and corners. Welding also burns away local zinc, so those areas require suitable repair treatment. It is not a universal answer. That assumption can fail.
Engineers should check coating thickness, forming requirements, drainage, and the surrounding environment before selecting the coil. Thin condensation trapped between overlapping sheets may still create problems. Good detailing matters. Oversight is common.
Why Choose Hot Dip Galvanized Steel Coil?
What Factors Should Guide Your Selection?
The right galvanized steel coil depends on service conditions, not appearance alone. Start with the environment. Coastal air, industrial fumes, moisture, and indoor dryness create very different corrosion risks. Environment changes everything. A thicker zinc coating usually offers longer protection, but it may increase cost and affect forming behavior.
Check the coating designation and thickness carefully. Ask for test reports, dimensional tolerances, and mechanical property data. These records help confirm whether the coil matches your drawings and production process. Coil width, thickness, yield strength, and elongation should fit the intended forming method. Deep drawing needs different performance from simple bending. Do not guess.
Surface quality also matters. Examine the coating for bare spots, heavy deposits, scratches, or uneven zinc patterns. Small defects can become visible after painting or stamping. In practical purchasing, I have seen projects focus on price while overlooking storage conditions. That decision often creates white rust before fabrication begins. Keep coils dry, ventilated, and protected from trapped condensation. Measure twice.
Consider the final application as well. Welding, cutting, painting, and roll forming may require specific coating levels or steel grades. Confirm compatibility with your equipment before ordering large quantities. Relevant inspection standards can improve consistency, but paperwork alone is not enough. Sample testing remains valuable, especially when suppliers, batches, or processing temperatures change. A reliable selection balances corrosion resistance, formability, surface quality, availability, and total processing cost.
© 2025 Messer Cutting Systems, Inc.