How to Prototype Sheet Metal Parts?
Prototype Sheet Metal parts turn a digital design into a physical test of fit, function, and manufacturability. A flat CAD drawing may look convincing, yet a bend can shift a hole or leave too little room for a fastener. The prototype makes these details visible. Quickly.
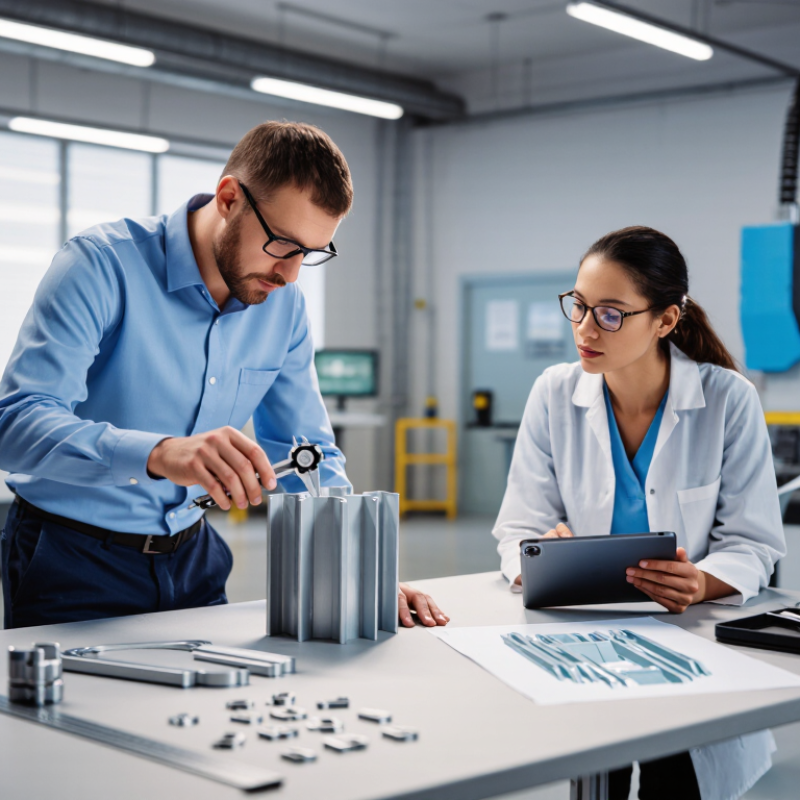
A practical process starts with the part’s purpose, material, thickness, and critical dimensions. Engineers then check the flat pattern, bend radii, reliefs, and likely tool access before cutting a blank. Laser cutting can produce accurate profiles, while a press brake forms the bends. Edges may need deburring, and the finished part should be checked against the drawing with calipers or a simple fit test. Small steps matter.
Testing should focus on real use, not appearance alone. Does the panel align with its mating parts? Can a technician reach the screws? Does the enclosure flex when a connector is installed? These checks can reveal problems before a design moves toward production. Still, one prototype rarely answers everything. A hand-formed sample may not behave exactly like a larger production run, and that difference deserves attention.
This guide explains how to plan, fabricate, and evaluate sheet metal prototypes, including material selection, design preparation, forming, and inspection. It also considers common trade-offs between speed, cost, and accuracy. The process is iterative. A measured revision often teaches more than a polished model.
Define the Requirements for the Sheet Metal Prototype
Before modeling a sheet metal prototype, define what it must prove. Is the goal to check fit, stiffness, appearance, or assembly sequence? Write down the critical dimensions, mating surfaces, load direction, and test conditions. For a bracket, that might mean a 2 mm sheet, two mounting holes, and a specified load at the free end. Separate must-have limits from dimensions that can vary. Otherwise, a prototype may look right but fail at assembly.
Specify material, thickness, bend radii, hole locations, finish, and acceptable edge condition. Note whether the part will be laser-cut, punched, or formed, since each process can affect features and tolerances. The 2021 manufacturing skills-gap study projected that 2.1 million U.S. manufacturing jobs could go unfilled by 2030. That makes clear drawings and straightforward inspection especially valuable when specialist time is limited. Include a simple inspection plan: identify datums, list the few dimensions that determine fit, and state how they will be measured. A caliper check may suit a prototype; it may not reveal springback across a long flange. Be specific, but leave room to learn. Early requirements are sometimes wrong. Revise them when test results show the part behaves differently than expected.
How to Prototype Sheet Metal Parts: Define the Requirements
Choose a material and thickness before detailing bends, tolerances, and inspection criteria. The chart shows nominal thicknesses for common U.S. standard steel sheet gauges.
Prototype planning tip: Specify thickness in millimeters or inches on the drawing, as gauge numbers can vary between materials and standards. A lower gauge number indicates thicker steel.
Select the Material and Forming Processes
Material selection should start with the part’s job, not a favorite metal. A thin cover may need easy bending and a clean finish, while a bracket needs stiffness around its mounting holes. Aluminum is light and often straightforward to form; mild steel is tougher but heavier. Stainless steel can resist corrosion, though its springback may surprise you. Check the alloy, temper, and sheet thickness together. They affect how a bend behaves.
Match the prototype process to both the shape and the expected production method. Laser cutting works well for outlines and hole patterns, especially when dimensions may change. A press brake can form flanges and simple bends without dedicated tooling. For repeated, complex parts, stamping may better reflect production, but the tooling takes time and cost. Keep bend radius, relief cuts, and grain direction in mind. Small details matter. A narrow flange can crack if the radius is too tight for the chosen material.
A useful prototype is not always the prettiest one. It should reveal whether the part fits, assembles, and survives its intended use. If production will use a different alloy or forming process, note that gap clearly; the prototype may behave differently. It is easy to overlook springback on a quick first sample. Measure the formed angles, adjust the bend allowance, and record what changed. That record saves guesswork later.
Create the CAD Model and Flat Pattern
A sheet metal prototype starts with a model that describes how the part will actually be made. Set the material thickness, inside bend radius, and bend method before adding detailed features. Keep the thickness consistent unless the design requires a formed transition. A small mismatch can create a flat pattern that looks right on screen but will not fit the brake setup. Small details matter.
Use the CAD system’s sheet metal features for flanges, hems, and reliefs instead of modeling each bend as a solid block. Add bend relief near corners, and leave clearance where flanges meet. For a folded enclosure, check door gaps and fastener access in the formed model. A clean-looking design can hide a screw that a driver cannot reach. That is easy to miss.
Generate the flat pattern from the finished model, then inspect its bend lines, cutouts, and overall dimensions. Confirm the material thickness and bend allowance or K-factor with the shop’s tooling data; values vary by material and process. Check that holes stay clear of bend zones, and avoid narrow tabs that may distort during forming. A paper print or cardboard fold can reveal awkward geometry before cutting metal. It is not a substitute for a real trial, but it catches obvious errors. If the first formed part differs, revise the bend data and record what changed. Some estimates will be wrong. That is useful feedback.
Fabricate the Sheet Metal Prototype
To fabricate a useful sheet metal prototype, start with the part’s job, not just its shape. Define loads, mounting points, material, thickness, and critical dimensions before creating the flat pattern. Allow for bend relief and confirm the inside radius with the actual tooling; a guessed bend allowance can shift hole locations. Cut one blank, deburr its edges, then form it on a press brake. Check the first part with calipers and a square. Small errors show quickly.
A 2024 Grand View Research industry report estimated the global sheet metal fabrication services market at USD 13.2 billion in 2023, reflecting broad demand for fabricated components. That scale makes repeatable prototype checks valuable, but it does not guarantee production fit. Use the intended alloy and thickness where possible, and record tooling, bend sequence, and measured dimensions. If the part needs welds, include them in the prototype; heat can pull a flat panel out of alignment. A first bend can still be wrong. I would inspect it before cutting a batch, even a small one, and revise the drawing when measurements disagree with the model.
Inspect the Part and Refine the Design
After forming a sheet metal prototype, inspect the part under good light before changing the design. Check overall dimensions, bend angles, hole locations, and edge condition against the drawing. A caliper can reveal a hole that shifted slightly, while a square helps spot a bend that is not quite 90 degrees. Look closely. Small clues matter.
Do not judge the part by appearance alone. Assemble it with nearby components and check for interference, uneven gaps, and fastener access. Pay attention to springback: a bend may look correct on the bench but open slightly after the forming force is removed. On one early prototype, the exterior looked clean, yet a flange blocked a neighboring panel. That miss was useful, though it should have been caught sooner. Record measured deviations, not just impressions, then adjust bend allowances, reliefs, or clearances in the model.
Tips: Photograph the part beside a ruler, mark problem areas, and compare measurements with the flat pattern. Change one feature at a time when possible. This makes cause and effect easier to track. Recheck material thickness and grain direction before revising a bend. If the prototype still fits poorly, revisit the design assumptions rather than forcing the part into place.